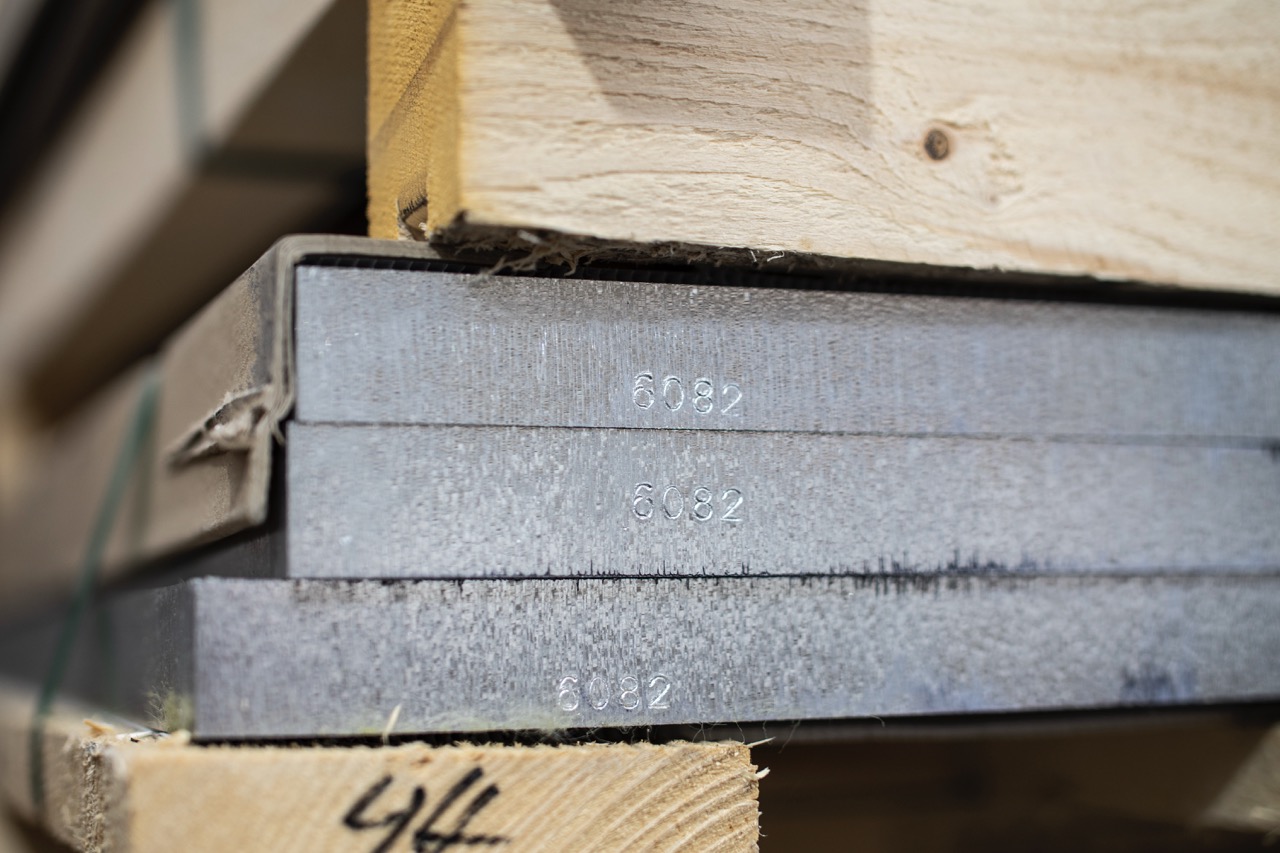
The most widely usable alloy grade, characterised by medium or slightly higher strength. It machines, welds and anodises well.
(EN 573-3)
| Specifications (%) Remainder: Aluminium |
Others | ||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Si | Fe | Cu | Mn | Mg | Cr | Ni | Zn | Ti | Ga | V | Notes | Each | Total2 |
| 0,70 - 1,30 | 0,50 | 0,10 | 0,40 - 1,00 | 0,60 - 1,20 | 0,25 | - | 0,20 | 0,10 | - | - | - | 0,05 | 0,15 |
The values and data below are indicative – they help to give a general picture of the material.
| EN AW | Al Si1 Mg Mn |
|---|---|
| Old designation | Al Mg Si1 |
| Material number (DIN) | 3.2315 |
| United Kingdom (BS) | H30 |
| Italy (UNI) | 9006/4 |
| Spain | L-3453 |
| Sweden | 144212 |
| Norway | - |
| France (AFNOR) | A-SGM0,7 |
| Colour code | RAL 5010 Gentian Blue |
| Density [g/cm3] | 2,70 |
|---|---|
| Modulus of elasticity [GPa] | 70,0 |
| Thermal conductivity [W/m*K] | 170 – 220 |
| Thermal expansion coefficient [K-1*10-6] | -50°C – 20°C |
| 20°C – 100°C | 23,4 | |
| 20°C – 200°C | |
| 20°C – 300°C | |
| Specific heat [J/(kg*K)] | 896 |
| Electrical conductivity [m/Ω*mm2] | 24 – 32 |
| Shear modulus [GPa] | 26,4 |
| Annealing / recrystallisation annealing | |
|---|---|
| Annealing temperature | 380°C – 420°C |
| Heat-up time | 1 – 2 hours |
| Cooling conditions | ≤ 30°C/hour to 250°C, air below 250°C |
| Hardening | |
|---|---|
| Solution heat treatment | 525°C – 540°C |
| Quenching | water · air |
| Natural ageing | 5 – 8 days |
| Artificial ageing | 155°C – 190°C · 4 – 16 hours |
| Machinability | |
|---|---|
| Annealed | 4 |
| Work-hardened | - |
| Heat-treated | 2 |
| Dimensional stability | 3 – 4 |
| EDM | 1 |
| Surface treatment | |
|---|---|
| Anodising – (protective anodising) | 1 |
| Special anodising quality (EQ)EQ | - |
| Anodising – decorative | 3 |
| Painting / coating | 2 |
| Polishing | 1 – 2 |
| Weldability | ||
|---|---|---|
| Process | Value | Filler metal |
| Gas | 3 | SG-Al Mg4 |
| TIG | 2 | SG-Al Mg4,5 Mn |
| MIG | 1 | SG-Al Si5 |
| Resistance welding | 3 | - |
| Solderability | |
|---|---|
| Brazing with flux | 3 – 5 |
| Brazing without flux | 4 |
| Abrasion soldering | 2 |
| Soft soldering with flux | 3 |
| Corrosion resistance | |
|---|---|
| In a normal atmosphere / weathering conditions | 1 |
| Marine air environment | 2 |
| Formability | ||
|---|---|---|
| Cold forming | Value | Delivery temper |
| Bending | 3 | T3 · T4 |
| Compression forming | 2 | O |
| Deep drawing (temper-dependent) | 2 | O |
| Upsetting (temper-dependent) | 2 | O |
| Impact extrusion | 2 | O |
| Hot forming | Value | |
|---|---|---|
| Closed-die forging | 2 | |
| Extrusion | 2 | |
| Hammer forging | 2 |
| Suitable for food contact (according to DIN EN 602) | yes |
|---|
| Service temperatures |
Long term approx. 120°C – 135°C Short term approx. 155°C – 170°C |
|---|
DIN EN 485-2:2009-01
EN 485-2:2008
Below LV=10 mm the flatness parameters are not guaranteed!
| Temper | Nominal thickness t [mm] |
Tensile strength Rm min. [MPa] |
Proof strength Rp0,2 min. [MPa] |
Elongation A50 min. [%] |
Bend factor 90° r ≈ k · tb |
Hardness HBWa |
|---|---|---|---|---|---|---|
| T651 | 6,0 – 12,5 | 300 | 255 | 9 | 6,0 · tb | 91 |
| 12,5 – 60,0 | 295 | 240 | 8 | — | 89 |
Notes:
a) HBW: Brinell hardness (carbide ball, test according to the standard).
b) t: plate thickness; bend radius is an indicative value.